Refacing valve seats
WIS 05-155
Data Intake
Exhaust
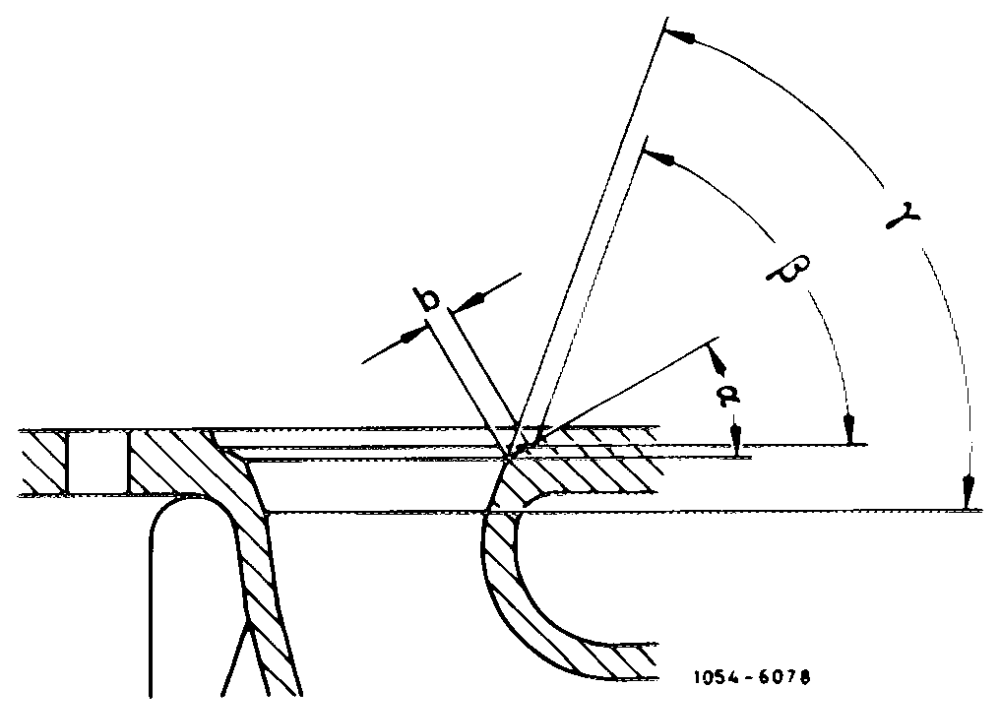
Valve seat width b 1.3–1.6 2.5–2.9
Valve seat angle a
60° Correction angle top B
Correction angle bottom y acc. to shape of casting
Permissible runout of valve seat 0.03
Minimum distance ‘’a aa with new valves and new valve seats
ET Le VLLLLCLLOLI YK SS Intake +0,03 to -0.43
Exhaust -0.38 to -0.78
Maximum distance ‘‘a’’ with new valves sage
and refaced valve seats
Intake -1.5 Exhaust
The maximum distance drops by the same amount as the cylinder head parting surface is refaced.
Special tools
a \ ZF Valve adjusting wrench 14 mm (two) Holding wrench for valve spring cap – 615 589 00 03 00
Installer for valve stem seals, intake and exhaust – 617 589 00 43 00
Plug gauge 10 mm dia. for intake and exhaust valve guides – 615 589 00 21 00
. . . e.g. Christ, 6801 Neckarhausen Cylinder head clamping fixture order No. DBK 60–2 f
| Val alve seat borer | e. g. Hunger, 8000 Miinchen type VDNSL 1/45/30, order No. 236.03.308 |
| Tester for valve seats | e. g. Hunger, 8000 Miinchen order No. 216.93.300 |
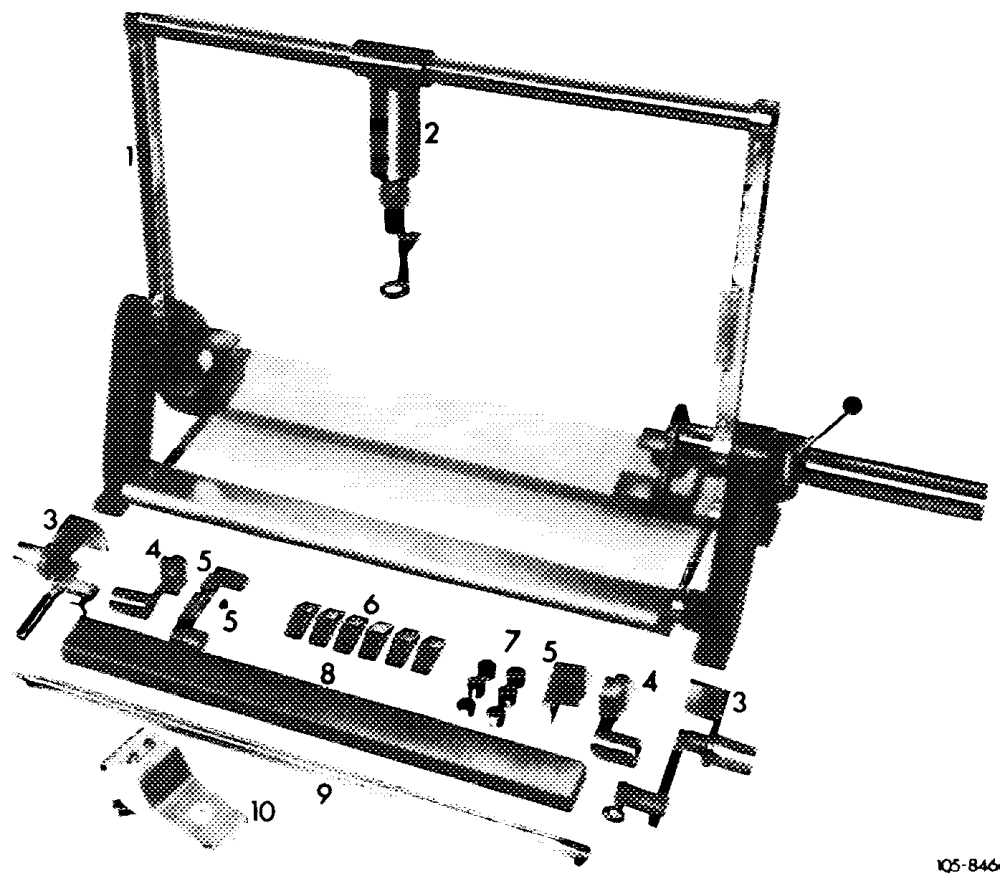
Mount cylinder head in clamping fixture for disassembly and treatment.
Reface valve seats with valve borer, valve grinder or valve cutter.
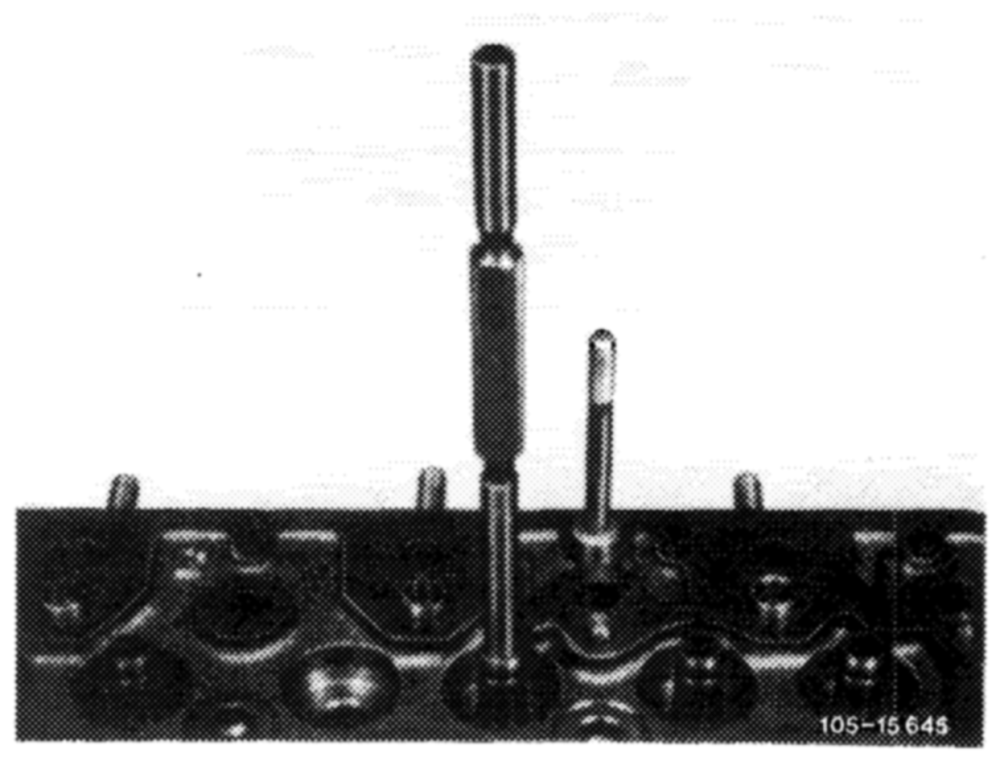
1 Check valve guides, replacing if necessary (05—135).
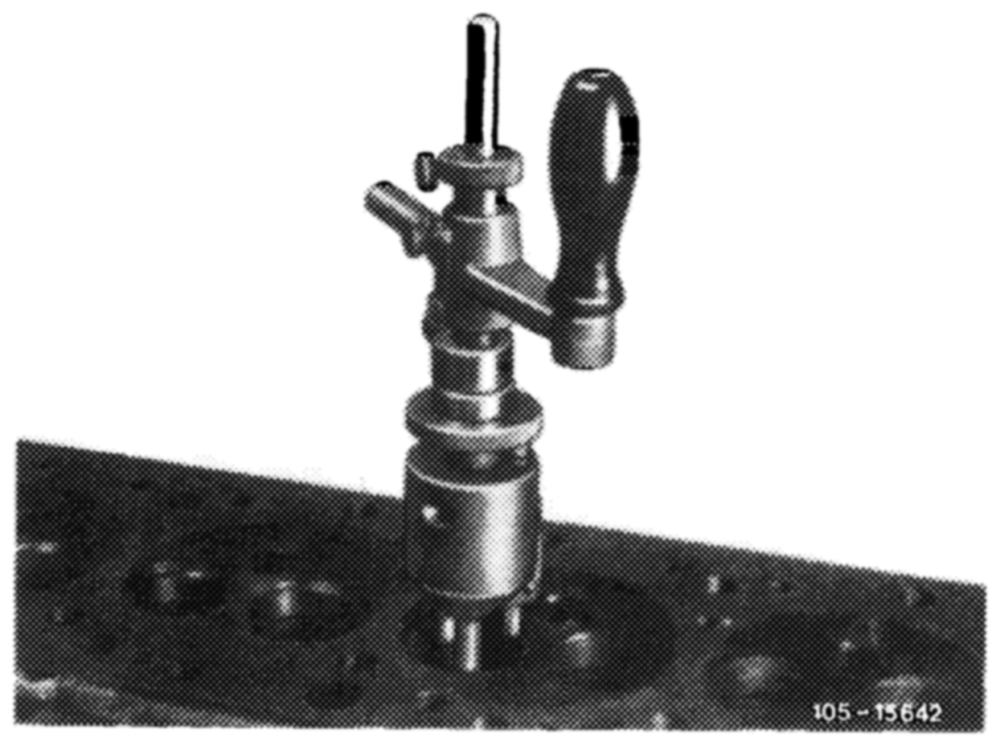
for use).
Caution: Do not release pilot (013) until valve seat runout has been checked.
3 Measure valve seat width b and, if necessary, correct angle at bottom in accordance with shape of casting.
If necessary, additionally increase undercut at 60°.
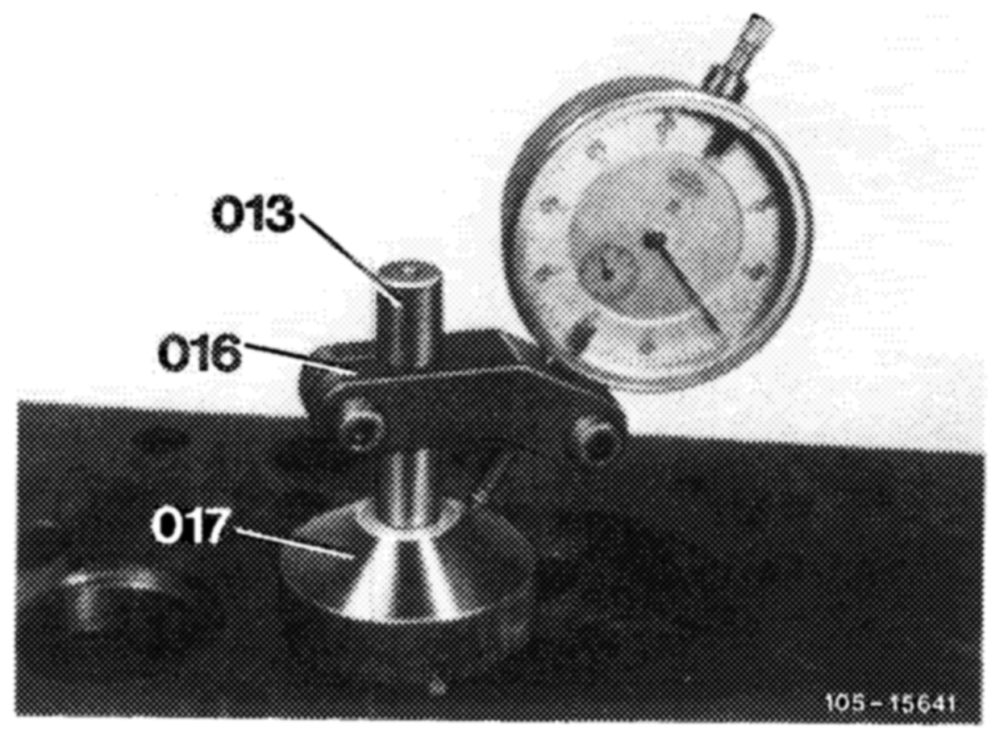
4 Check valve seat runout.
For this purpose slip testing sleeve (017) onto pilot (013), together with dial gauge holder (016) and dial gauge. Now turn testing sleeve, making sure that permissible runout of 0.03 mm is not exceeded.
013 Pilot 016 Dial gauge holder 017 Testing sleeve
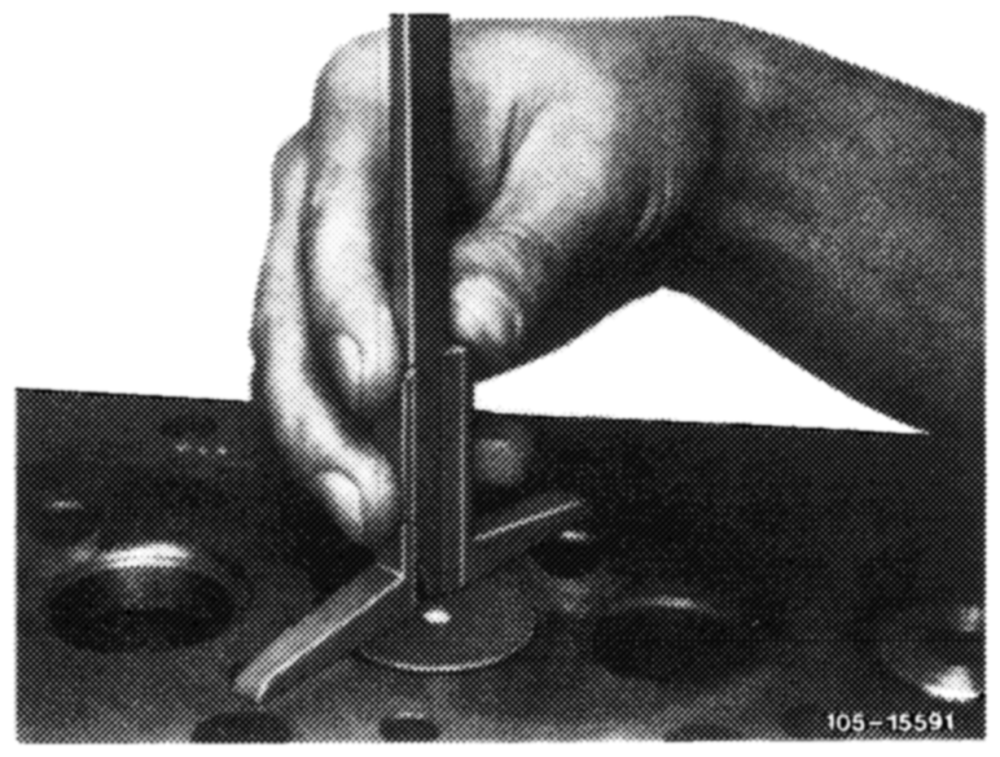
5 Insert new valve and measure maximum distance uae a.