Replacing valve seat rings
WIS 05-2900
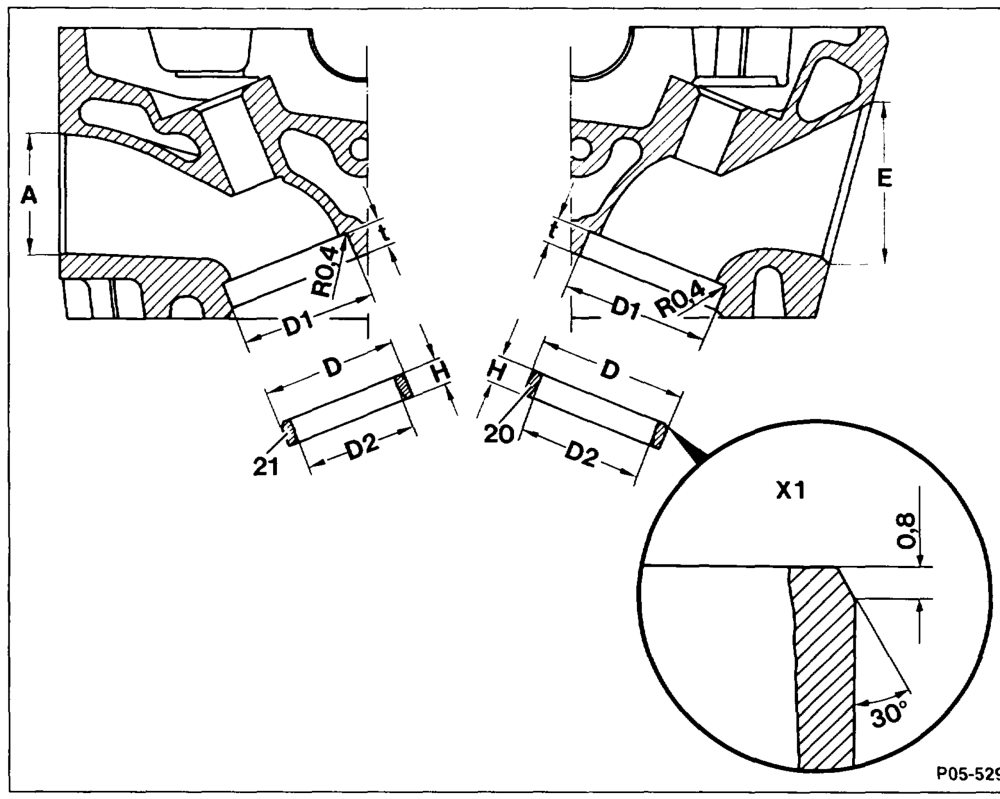
Preceding work: Valve guides checked (05-2130)
Valve seat rings (20 and 21) remove with ring seat turning tool. Operating instructions of tool manufacturer
note. Basic bore dia. (D1) measure with internal measuring instrument. Valve seat rings (normal size or repair size) select according to overlap. For repair Size 1. eee eee machine basic bore.
For repair size machine valve seat rings according to basic bore in cylinder head, pay attention to overlap. For repair size turn chamfer (X1) on valve seat rings. Valve seat ring cool with liquid nitrogen and knock in with suitable drift. Valve seats machine (05-2910).
wae =RA 05.1123-2900/1
103.98
Engine
103.94
| Valve seat ring | Inlet | Exhaust | Inlet | Exhaust | |||
| D1 | Standard size | 42.50 – 42.52 | 37.50 ~ 37.52 | 45.50 – 45.52 | 41.50 – 41.52 | ||
| D | Standard size | 42.59 — 42.60 | 37.59 -37.60 | 49.59 – 45.60 | 41.59 – 41.60 | ||
| Overlap of valve seat rings in cylinder head | 0.07 – 0.10 | 0.07 – 0.10 | |||||
| H | 8.12 – 8.20 | 8.12 — 8.20 | |||||
| t | 7.8 – 8.2 | 7.8 – 8.2 | |||||
| D2 | 36.2 | 31.2 | 39.2 | 35.2 | |||
Commercially available tools
Cylinder head clamping device eg. Hunger, D-81375 Munchen Order no. 221.60.000
Ring seat turning tool (size 2) eg. Hunger, D-81375 Munchen Order no. 220.03.110
Valve seat turning tool eg. Hunger, D-81375 Munchen Type VDSN 1/45/30, Order no. 236.03.308
Test kit for valve seats eg. Hunger, D-81375 Munchen Order no. 216.93.300
Internal measuring instrument (range 35 – 100 mm)
External micrometer (range 25 – 50 mm)