Checking and machining valves
WIS 05-280
Data Intake valve Exhaust valve
| retainer Valve dia. | 39.7–39.9 | 34.1–34.3 | ||
| Valve stem dia. | 9.92–9.94 | |||
| Valve length | 131.5 | |||
| Code number on stem end | E617 00 | A 617 00 27 | ||
| Filled-in sodium | without | with | ||
| Valve seat plating | valve seat nitride-hardened | |||
| Height ‘‘h’’ of valve retainer | when new | 2.54 | 2.49 | |
| limit value | 2.0 | 2.0 | ||
| Adjusting angle for machining valves | 30° + 15° | |||
| Permissible runout at valve stem and valve seat max. | 0.03 | |||
| Valve shaft wear (wear limit) | 0.05 | |||
| Conventional tools | re | |||
| Valve cone grinder or valve cone machining tool | e.g. made by Matra-Werke GmbH D-6000 Frankfurt/Main 8 e.g. made by Hunger, D-8000 Miinchen | |||
Note Exhaust valves are filled with sodium.
When scrapping valves, pay attention to safety rules. Do not melt valves filled with sodium, since there is a risk of explosion, and do not use such valves for making tools (punch, etc.), without first removing filled-in sodium.
Be careful when removing sodium from valve, since sodium mixed with water and watery solutions reacts heavily explosive, while the resulting hydrogen gas may cause fires.
Sodium from cut-up or broken-up valves can be neutralized in a mixture comprising 2 liters of spirit of alcohol and 1 liter of water put into a vessel and placed in the open air.
Valves filled with sodium can be collected and shipped for neutralizing to: Garantieprisfstelle Werk Stuttgart-Untertirkheim.
Checking and machining . a nh. 1 @
1 Clean valves and check visually.
Valves with a burnt valve retainer, with insufficient 2-3662 height ‘‘h’’ of valve retainer and valves with worn out or scored valve stem should be replaced.
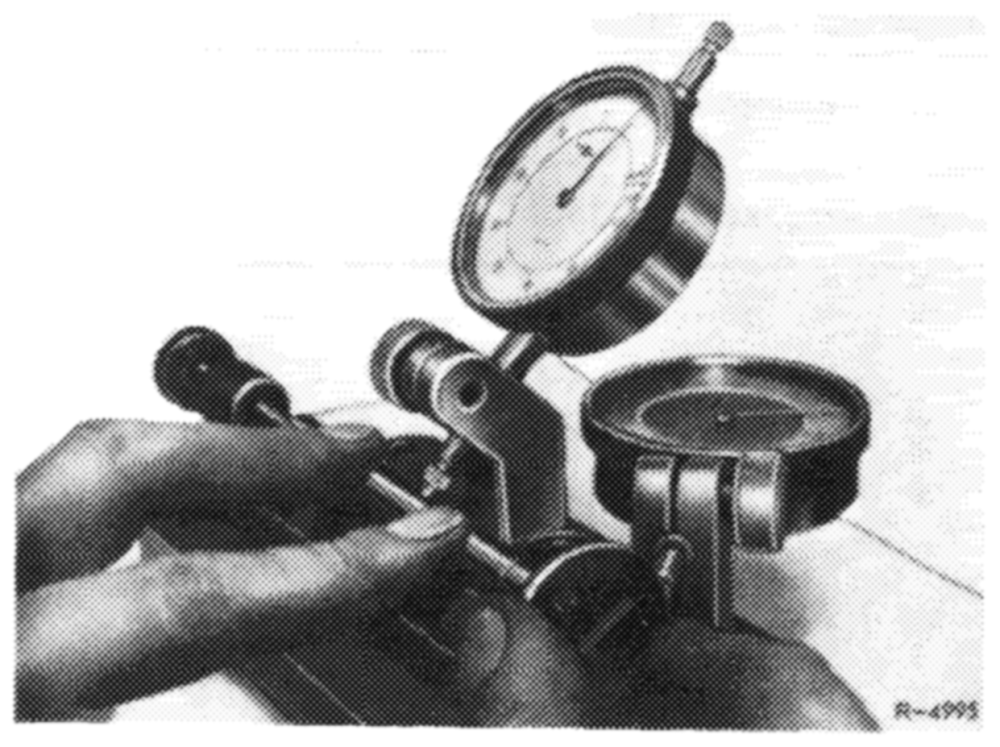
2 Measure runout on valve stem. If runout exceeds 0.03 mm, replace valve.
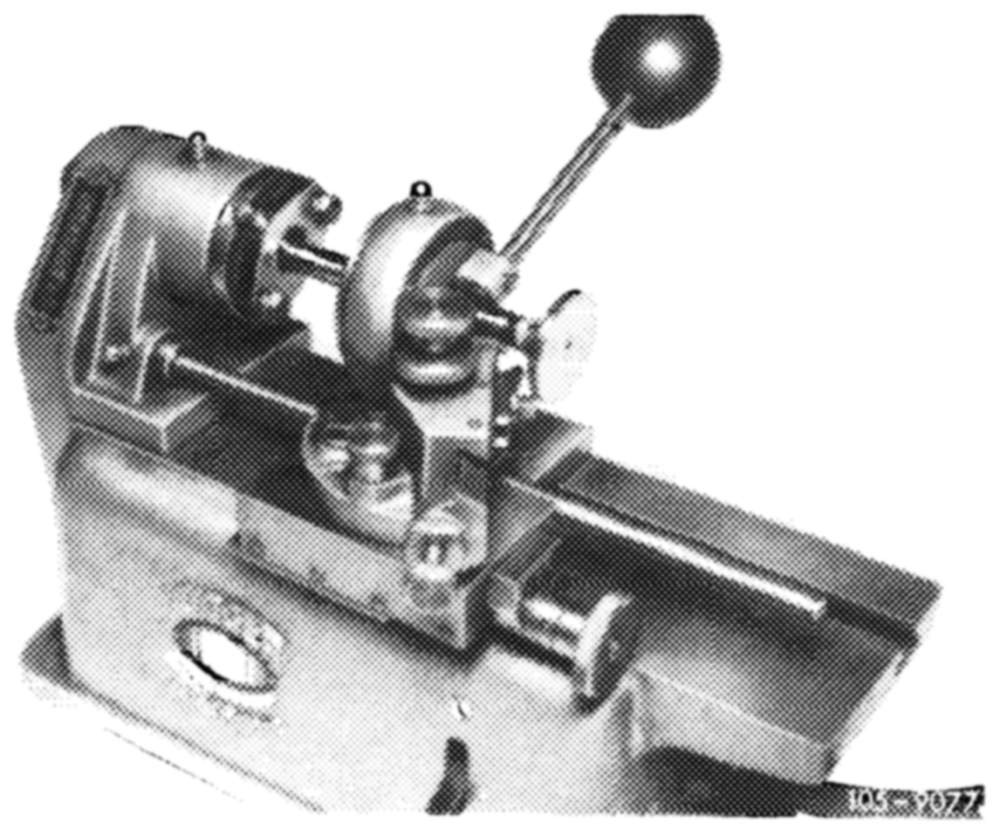
3 Machine valve seat.
Refer to operating instructions of machining tool and make sure of a 30° adjusting angle.
4 Measure runout on valve seat and height ‘‘h’’ of valve retainer.
As soon as the limit values are attained, replace valve.