Checking and refacing valves
WIS 05-280
Data Intake valve Exhaust valve Engine _ 615 616, 617 615 616,617 Valve head dia. 38.7–38.9 39.7–39.9 33.1–33.3 34.1–34.3 Valve stem dia. a 9.92–9.94 Valve length 131.3–131.7 130.8-131.2 Code in stem end E 61501 E 616 02 A 615 04 A 616 05
Sodium filling none
Valve seat casing nitrided in bath
2.34 2.01 as new Heigth ““h” of valve head tolerance limit
30° + 15’ Adjusting angle for valve refacing
Permissible eccentricity at valve 0.03 stem and valve seat max.
Commercially available tools
Valve head grinder e.g. Matra-Werke GmbH 6000 Frankfurt/Main 8 or e.g. Hunger, 8000 Miinchen valve head cutter
1 Clean valves and sight-check.
All valves with burnt cylinder heads, with inadequate 2-3662 valve head height “‘h”’ and with worn or scored valve stems are to be replaced.
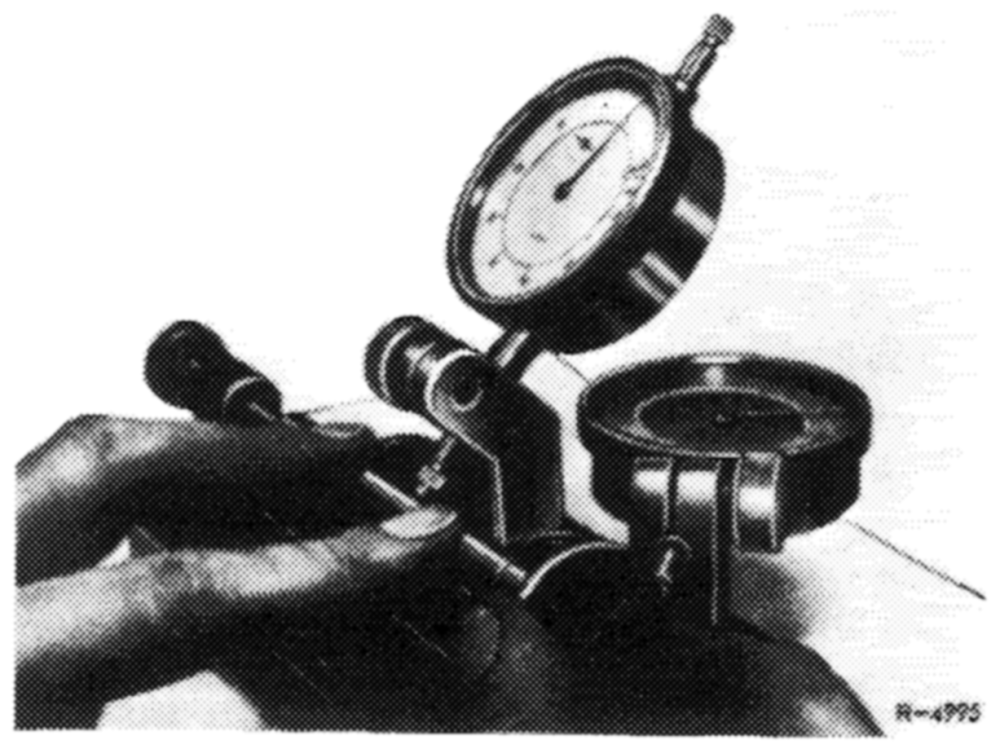
eccentricity exceeds 0.03 mm.
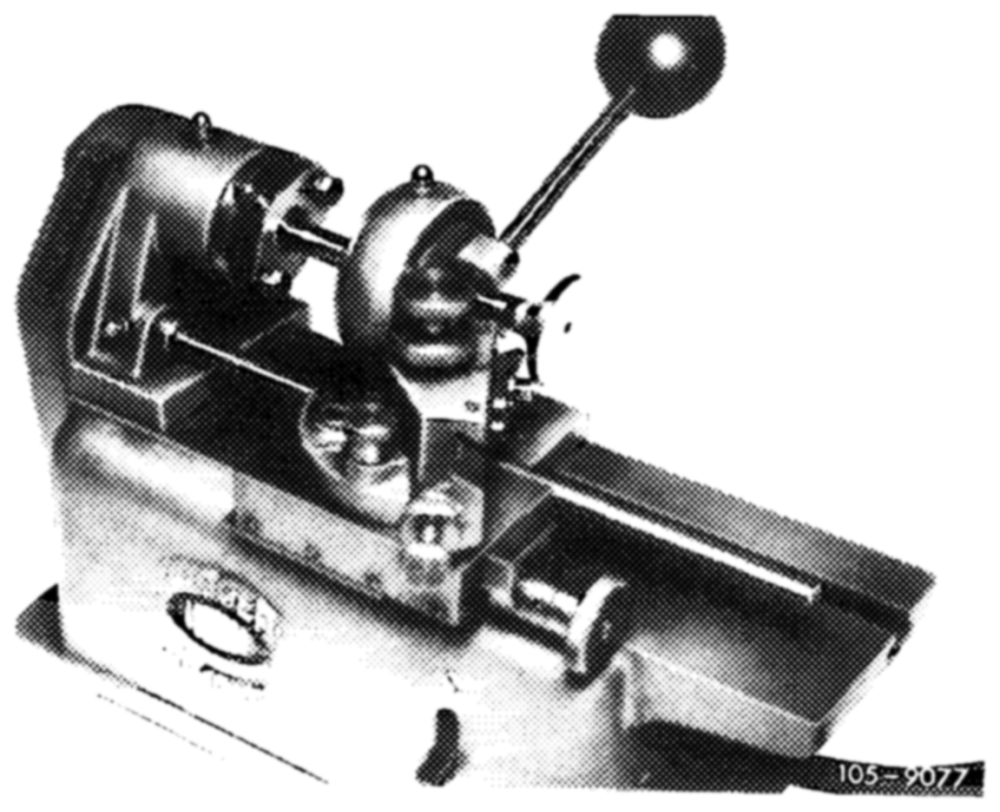
3 Reface valve seat.
Note instructions for use of machine, and adhere to 30° adjustment.
4 Measure valve seat eccentricity and valve head height “h’’.
Replace valve if tolerance limits are reached.