Refacing crankcase parting surface
WIS 03-015
Data
| Height of crankcase as new | 242.9–242.8 | ||
| Minimum height after necessary stock removal | 242.5 | ||
| Permissible irregularity of parting surface | lengthwise crosswise | 0.10 0.05 | |
| Permissible roughness of upper parting surface | 0.006–0.016 | ||
| Permissible parallel misalignment of upper to lower parting surfaces in lengthwise direction | 0.1 | ||
| Air testing pressure in water at bar positive | 1.4 | ||
| Cylinder bore chamber | see note | ||
| Gap between piston crown and crankcase | 615.913/940 Engines | +0.65 +1.05 to | |
| parting surface | Engines 615.912/941,616,617 | +0.50 to +0.90 |
Note
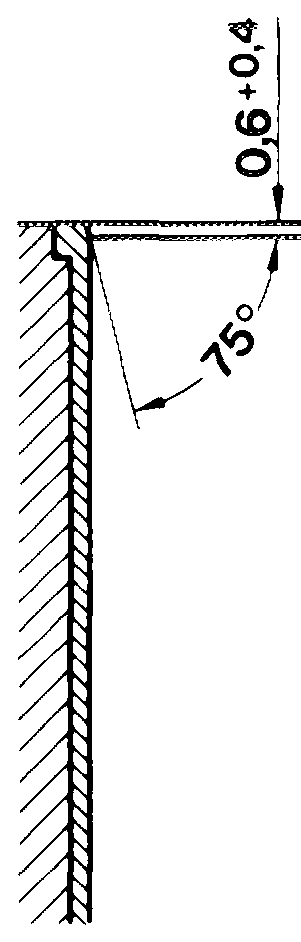
Prior to refacing, be sure to check piston projection. KKB This must not exceed 0.9 and 1.05 mm, respectively LELULLLLLELETLLLDELLELEDELILE, (03–316).
After refacing, be sure to chamfer cylinder bores.
\f crankcase parting surface has been refaced, valve timing will need re-adjusting (O5–215).
SLE 1034 ~ 8233