Repairing and aligning conrod
WIS 03-3130
Operation no. of operation texts and work units or standard texts and flat rates .
Engine 119.96 Engine 119.97/98
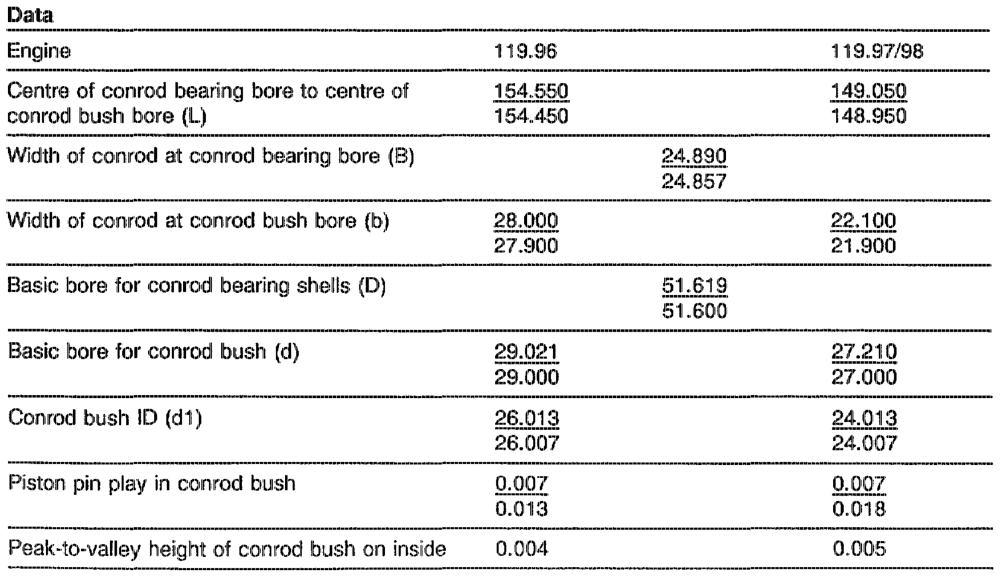
atmm RA 03.1921-3130/1
119.96 119.97 Permissible twist of conrod bearing bore relative 0.15 to conrod bush bore
Permissible variation of parallelism of conrod bearing bore to conrod bush bore
Permissible variation of conrod bearing bore 0.01 frorn roughness
Permissible difference in weight of complete 4g conrod within an engine
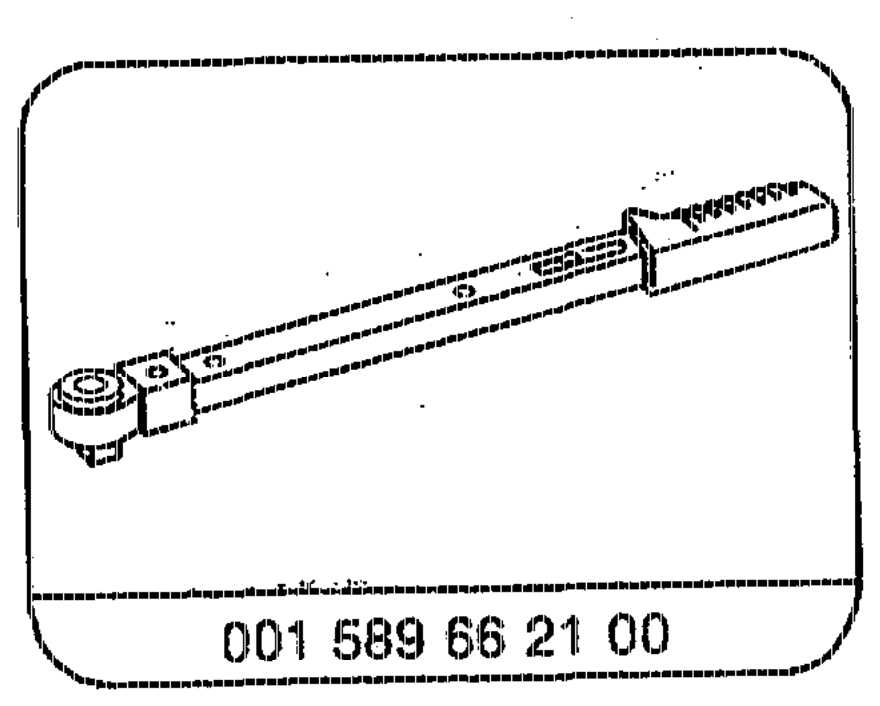
Special tool
Commercially available tools . Conrod tester g. Model BC 501 KWT D-6057 Dietzenbach
Conrod straightening device e@. g. Model BC 503 KWT D–6057 Dietzenbach
Quick-callipers for internal measurements dia. 20 – 40 mm dia. 40 ~ 60 mm
Micrometer 0–25 mm 50 – 75 mm
wih RA 03.1321-3130/2
Note Conrods which have been overheated as a result of the bearing damage (blue discolouring) must not be re-used.
Conrod and conrod caps are marked together. The conred stem must not have any transverse scoring and notches.
Conrods are supplied with machined conrod bush as a replacement part.
Conrod and crankshafts with different thrust collar dia. may be installed together when performing repairs.
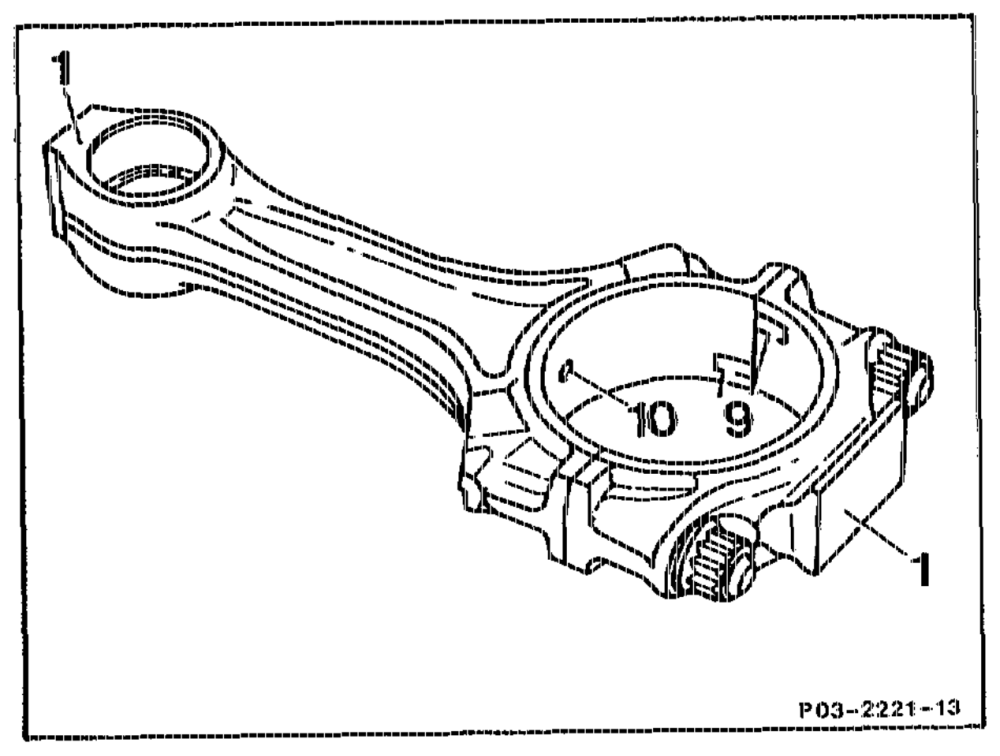
Engine 119.97: The conrod and the conrod cap ara fixed together with fit sleeves.
Pay attention to difference in weight when replacing the conrod.
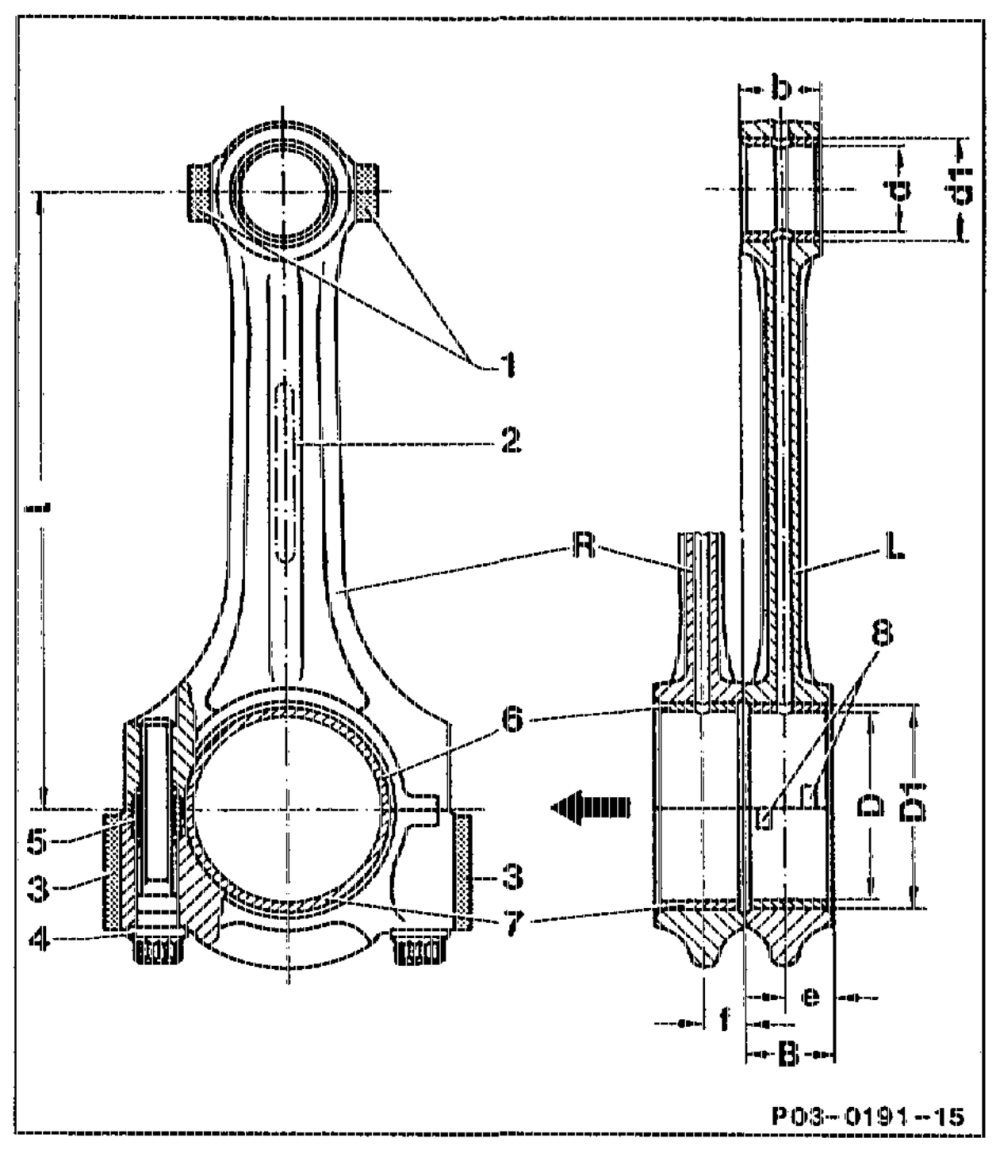
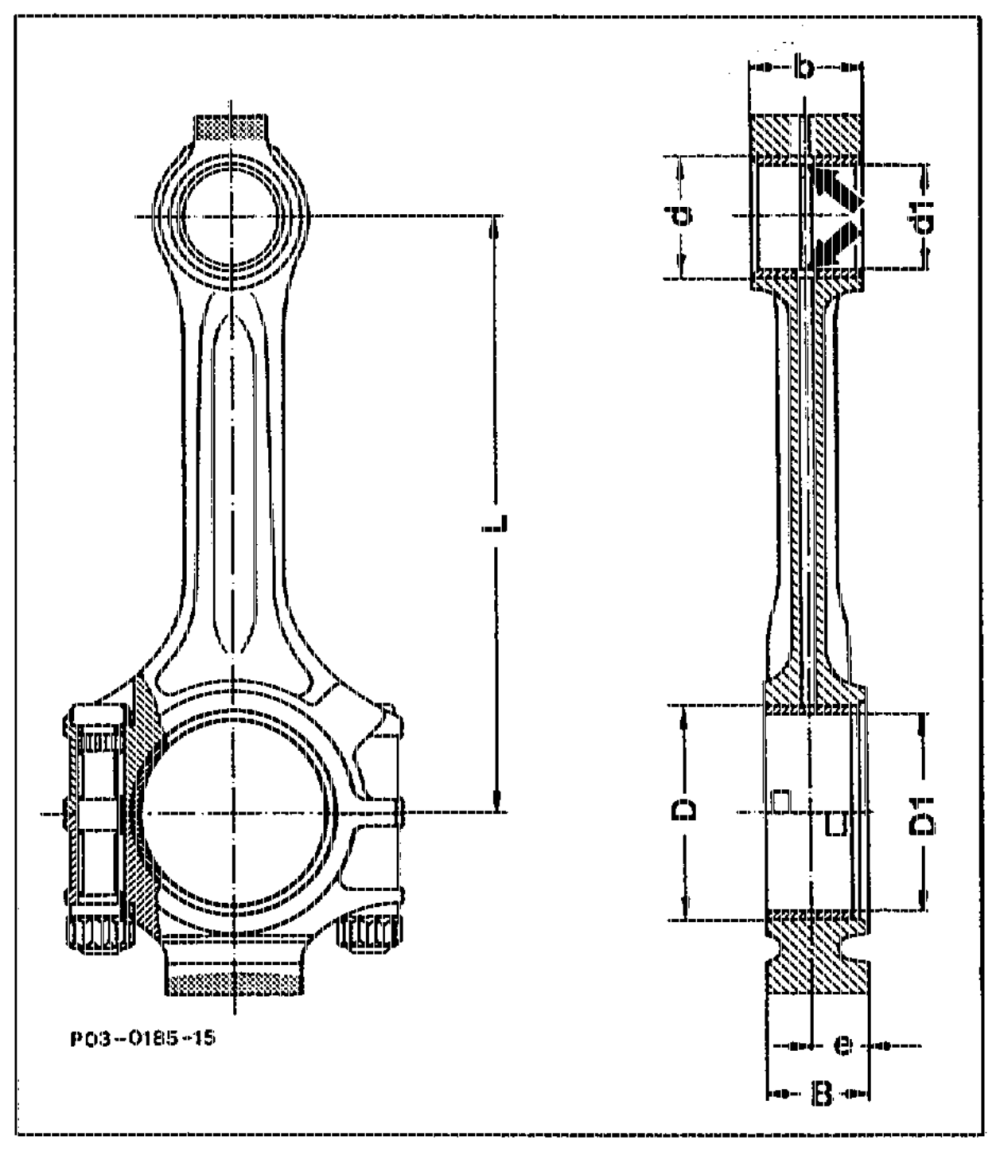
Conrod of engine 119.960 1 Weight balance 9 Locating grooves 10 Oil drilling
Repairing
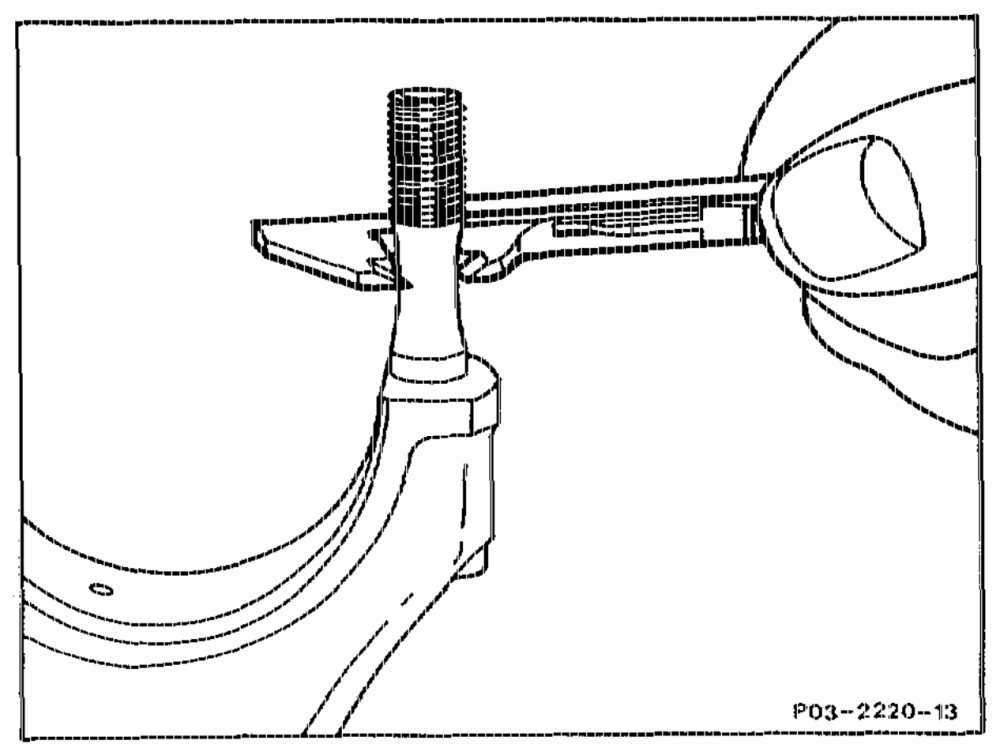
1. Check conrod bolts, replace if necessary (03-3100).
gts RA 03.1321-3130/3
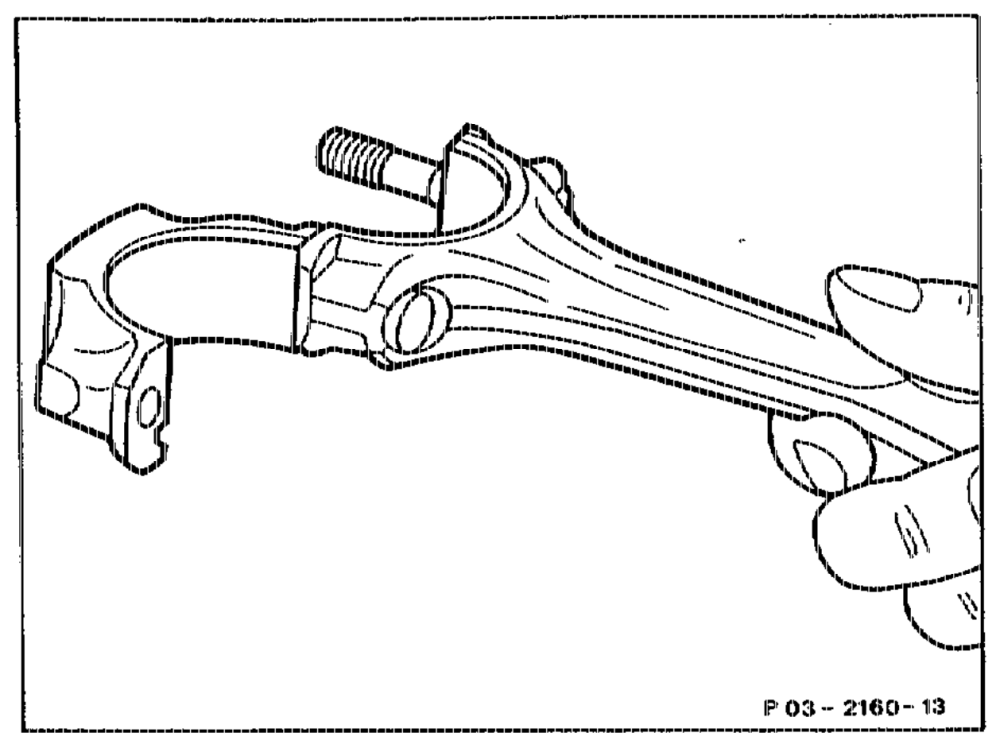
2 Engine 119.96: Examine bores for conrod bolts. Fit conrod cap onto a conrod bolt. ff the conrod cap moves down as the result of its own weight, the conrod must be replaced.
3 Install conrod bearing caps. Oil thread and bolt head contact surface for this step and tighten to 40 Nm. .
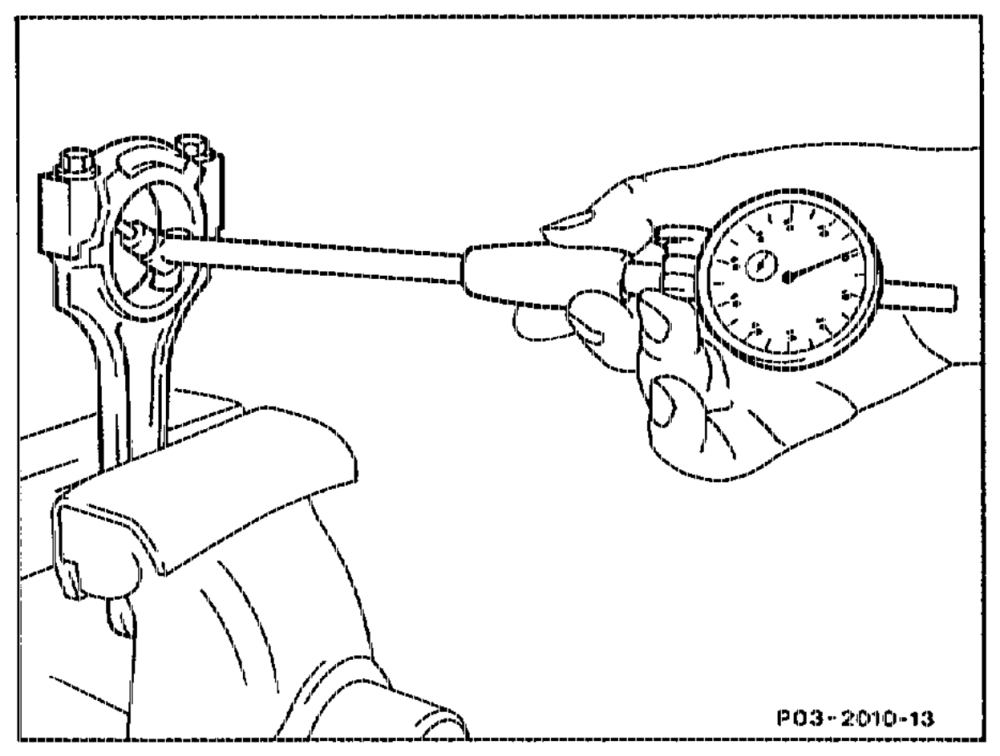
4 Measure conrod bearing basic bore. If the basic bore exceeds the value of 51.619 mm or is conical, dress bearing cover at its contact surface on a dressing plate up to max. 0.02 mrn.
5 Press in new conrod bush so that the oil bores are aligned (arrows). Insertion pressure 2500 N.
6 Turn or ream conrod bush.
7 Dress side contact surfaces of conrod on the dressing plate.
Conrod of Engine 119.96
aim RA 03.1321-3130/4
Aligning
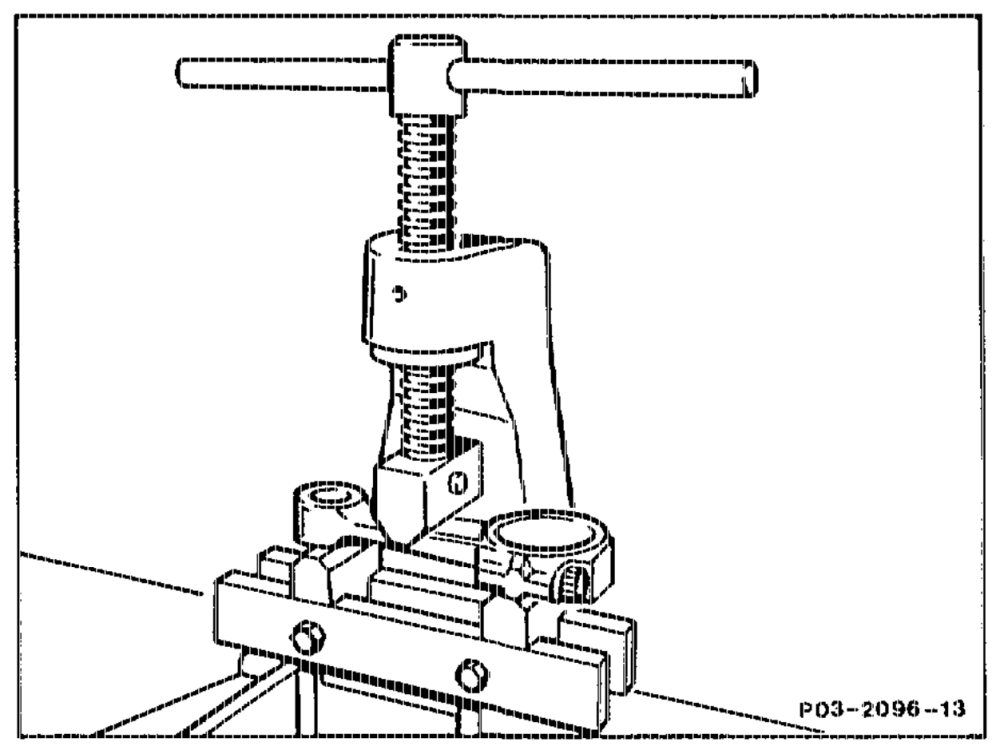
8 Align conrod with conrod tester.
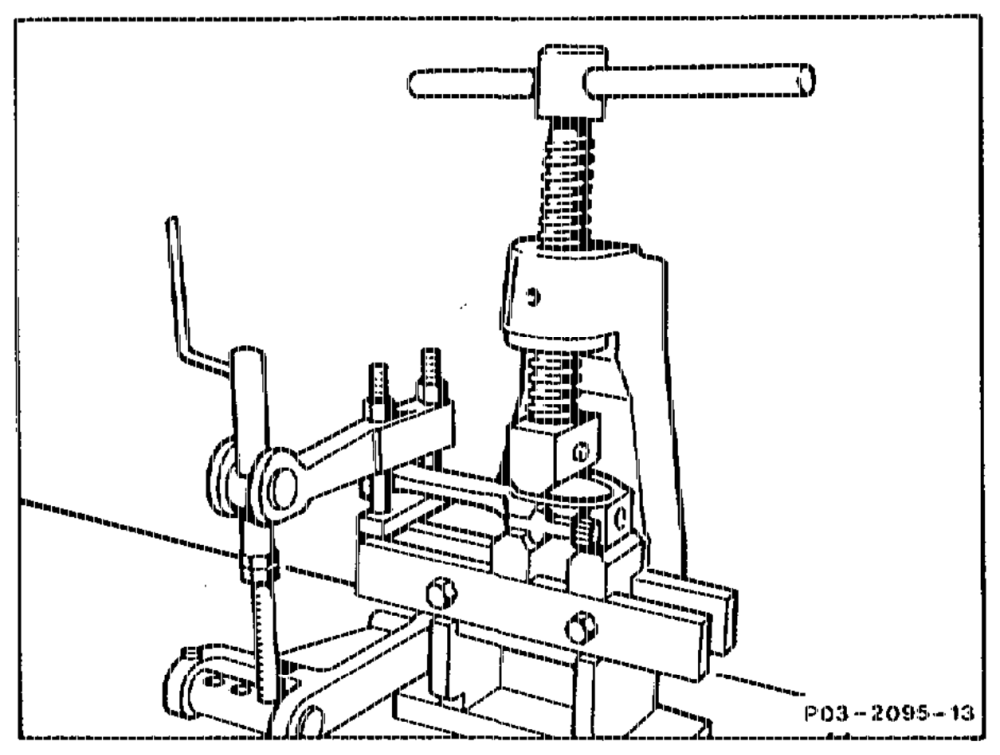
9 Align conrod bearing bore to conrod bush bore (parallelism).
10 Examine twist of conrod bearing bore to conrod bush bore and correct if necessary.
othe RA 03.1321-31390/5