Checking and machining valves
WIS 05-280
Intake valve Exhaust valve
Data
| Valve retainer dia. | 44.10–44.30 | 37.00–37.20 | |
| Valve stem dia. | 8.95–8.97 | 10.94–10.96 | |
| Valve length | 116.8–117.2 | 117.8-118.2 | |
| Code No. at shaft end | E 116 01 or E 116 02 | A 110 00 or 110 00 C | |
| Filled-in sodium | without | with | |
| Valve seat plating | with | with | |
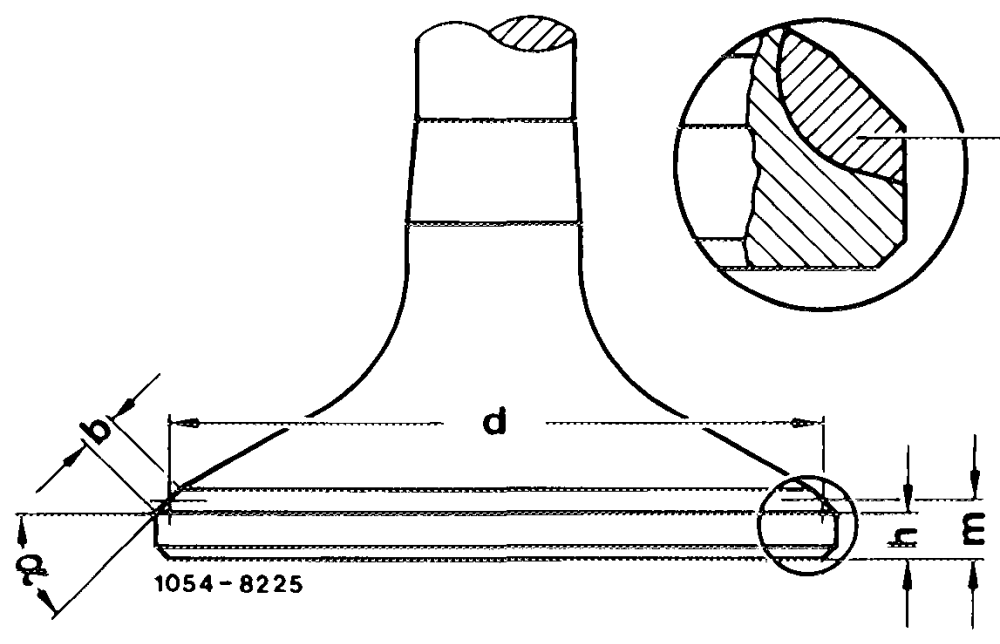
| . of valve | when new | 1.5 | 2.5 |
| Height reatiner Width “‘b” of valve seat | limit value | 1.0 1.8—-2.5 | 2.0 1.5–2.5 |
| Diameter ‘‘d” at valve seat center | 43.2. | 36.1 | |
| Height ‘‘m”’ up to valve | when new limit value | 2.1–2.3 1.6–1.8 | 3.1–3.3 2.6–2.8 |
| Adjusting angle for machining valves | 45° | ||
| Permissible radial runout vertically in relation to valve seat and on valve stem when mounted at valve stem | 0.03 | ||
| Permissible axial runout at end of valve stem when mounted at valve stem. | 0.015 |
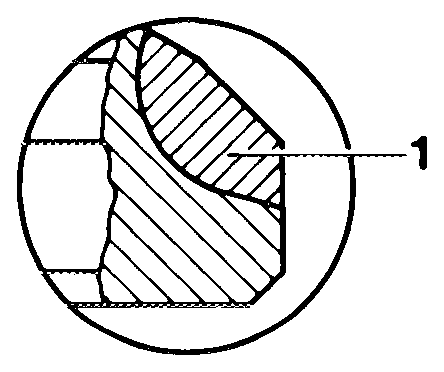
1 Valve seat plating
Conventional tools
Valve cone grinder e.g. Krupp, 0-5320 Bad Meckenheim model VS or Valve cone machining tools e.g. Hunger, D-8000 Miinchen 55, type VKDR 1, order No. 203.00.200
Note Exhaust valves are filled with sodium!
When scrapping valves, pay attention to safety rules. Do not melt valves filled with sodium since there is a risk of explosion and do not use such valves for making tools (punch etc.) without first removing filled-in sodium.
Be careful when removing sodium from valves, since sodium mixed with water and watery solutions reacts heavily-explosive, while the resulting hydrogen gas may cause fires.
Sodium from cut up or broken up valves can be neutralized in a mixture comprising 2 liters of spirit of alcohol and 1 liter of water put into a vessel and placed in the open air.
Valves filled with sodium can be collected and shipped for neutralizing to: Garantiepriifstelle Werk StuttgartUntertirkheim.
Ve
1 Clean valves and check visually.
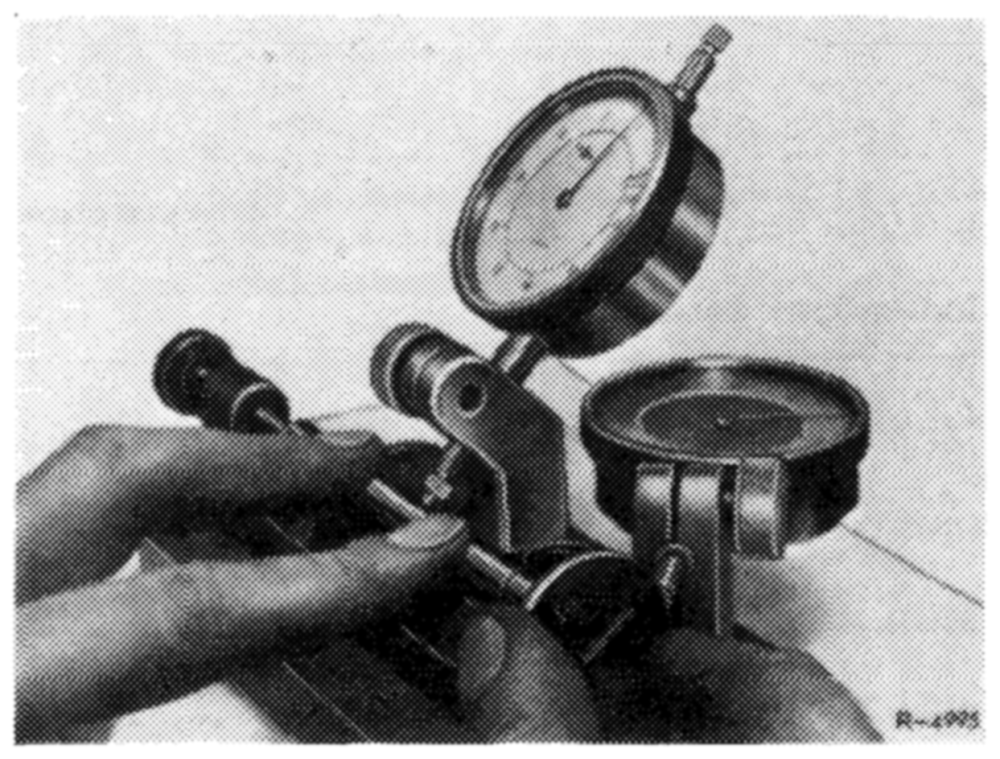
Valves with a burnt valve retainer, with insufficient 2-3642 height ‘’h’’ of valve retainer and valves with worn-out or score valve stem should be replaced.
2 Permissible radial runout at valve stem, check valve seat.
3 Check axial runout at end of valve stem.
Replace valve, if a limit value is attained.
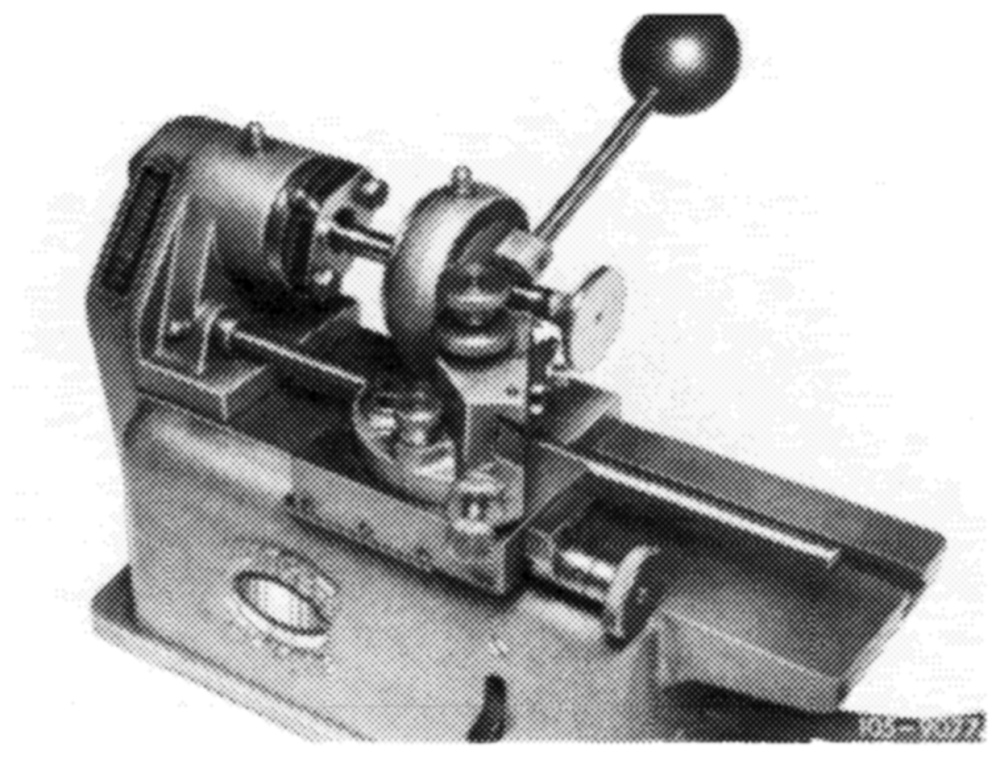
4 Machine valve seat and face of valve stem.
Refer to operating instructions of machining tool.
5 Measure runout on valve seat and height ‘’h”’ of valve disc.
When the limit values are attained, replace valve.